Send Inquiry
Reverse Osmosis (RO) Plant
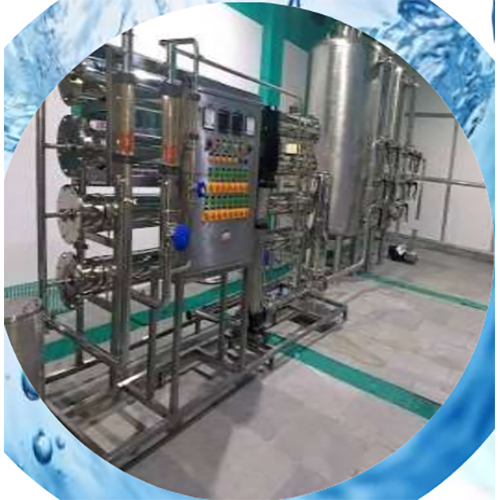

Reverse Osmosis (RO) Plant Specification
- Frequency
- 50-60 Hz
- Technology
- Reverse Osmosis Membrane Filtration
- Noise Level
- < 70 dB
- Feature
- Energy Efficient, Corrosion Resistant, User Friendly Panel
- Usage & Applications
- Drinking Water, Industrial Process Water, Boiler Feed, Pharmaceuticals, Food & Beverage
- Efficiency (%)
- Up to 99%
- Power Consumption
- 2 - 15 kW (Depending on Capacity)
- Water Out Conductivity
- < 10 S/cm
- Ph Level
- 6.5 - 8.5 (after treatment)
- Water in conductivity
- < 2000 S/cm
- Recycle Rate
- Up to 75%
- Flow Rate
- As per plant capacity (up to 10,000 LPH or more)
- Pump Type
- High Pressure Centrifugal Pump
- Purity Level
- Up to 99% removal of impurities
- Material
- Stainless Steel (SS304/SS316)
- Power Source
- Electric
- Drive Type
- Electric Motor
- Voltage
- 220-415 V
- Product Type
- Reverse Osmosis (RO) Plant
- Volume
- Customizable based on requirement
- Water Source
- Borewell, Tap Water, River Water
- Automatic Grade
- Automatic
- Filter Type
- Pre-Filter, Carbon Filter, Micron Filter, RO Membrane
- Capacity
- 250 LPH - 10000 LPH and above
- Installation Type
- Skid Mounted/Containerized
- Dimension
- Custom/As per client's requirement
- Maintenance
- Low, periodic membrane cleaning required
- Control System
- PLC Based Control Panel with HMI
- Safety Feature
- Low Pressure, High Pressure & Dry Run Protection
- Operating Temperature
- 5C - 45C
- Feed Water TDS
- Up to 2000 ppm (customizable)
- Design Pressure
- 8-15 kg/cm2 (Depending on application)
- Weight
- Varies with capacity e.g. 400 kg (for 2000 LPH unit)
- Membrane Type
- Polyamide, Thin Film Composite (TFC)
- Input Connection Size
- 1 inch - 2 inch (customizable)
- Skid Material
- Stainless Steel
- Recovery Rate
- Up to 75%
- Storage Tank
- Optional, Capacity as per requirement
Reverse Osmosis (RO) Plant Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 1 Unit Per Week
- Delivery Time
- 7 Days
About Reverse Osmosis (RO) Plant
Versatile Applications & Distinct Advantages
Our Reverse Osmosis (RO) Plant is ideal for a wide array of usages-ranging from drinking water to industrial process water, boiler feed, pharmaceuticals, and food & beverage sectors. The system's primary competitive advantages include energy efficiency, corrosion resistance, and customizable design, supporting capacities from 250 LPH to beyond 10,000 LPH. With advanced features and adaptable deployment on diverse application surfaces, it ensures unmatched water purity and reliability.
Hassle-free Policy, Prompt Supply & Markets Served
Experience seamless procurement with our RO Plant-stock ready and supported by a favorable sample policy and quick dispatch options. We ensure excellent supply ability and unwavering quality, catering to the competitive sale price demands of domestic and international markets. Our exports span across India and abroad, establishing us as a trusted solution provider committed to timely delivery and consistent client satisfaction.
FAQ's of Reverse Osmosis (RO) Plant:
Q: How does the Reverse Osmosis (RO) Plant ensure such high purity levels in treated water?
A: The plant uses polyamide, thin film composite membranes, along with a comprehensive multi-stage filtration system-including pre-filter, carbon filter, and micron filter-achieving up to 99% impurity removal and delivering unparalleled water quality.Q: What applications can this RO Plant be used for?
A: This RO Plant is versatile and suitable for drinking water production, industrial process water, boiler feed, pharmaceutical processes, and food and beverage manufacturing, making it a robust solution across many sectors.Q: What safety features are included in the RO Plant?
A: The plant incorporates low pressure, high pressure, and dry run protection to safeguard the system from operational hazards, ensuring reliable and secure daily operation.Q: How often does the RO Plant require maintenance?
A: Maintenance for the RO Plant is minimal, primarily involving periodic membrane cleaning. The stainless steel build and efficient control systems contribute to its low-maintenance operation.Q: Where can the RO Plant be installed and what are the installation options?
A: With customizable dimensions and skid-mounted or containerized installation options, the system can be configured for any facility, whether for indoor or outdoor placement, depending on client requirements.Q: What are the benefits of using this RO Plant in industrial setups?
A: Clients benefit from competitive pricing, reduced energy consumption, high efficiency, extended membrane lifespan, and consistent purity of water output, all of which contribute to lower operational costs and reliable process water supply.
Price:
- 50
- 100
- 200
- 250
- 500
- 1000+

More Products in Water Solutions Category
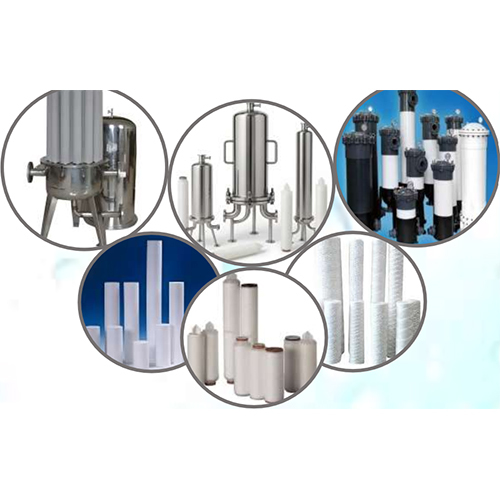
Micron Filtration Systems
Minimum Order Quantity : 1 Unit
Feature : High filtration efficiency, Easy to install, Corrosion resistant
Frequency : 50/60 Hz
Purity Level : Micron Level Filtration (0.1 to 50 microns)
Technology : Micron Filtration
Material : Stainless Steel, Polypropylene
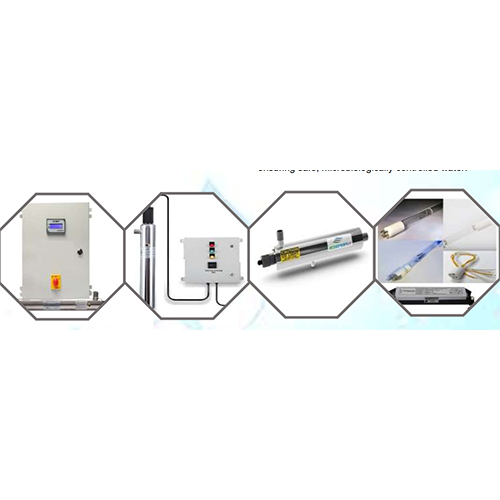
Ultraviolet (UV) Disinfection System
Minimum Order Quantity : 1 Unit
Feature : Chemicalfree disinfection, Low maintenance, Compact design
Frequency : 5060 Hz
Purity Level : 99.99% Pathogen Reduction
Technology : UVC Germicidal Irradiation
Material : SS304/SS316 Stainless Steel
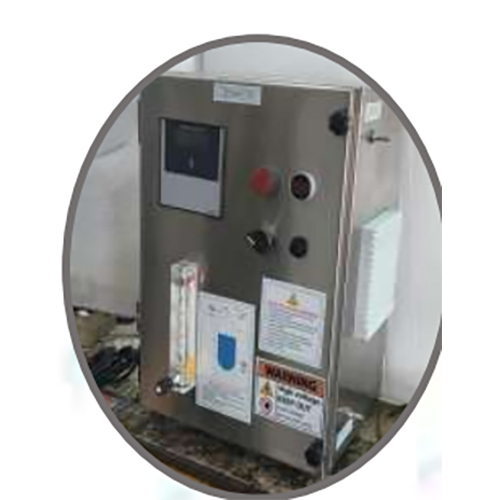
Ozone Generator
Minimum Order Quantity : 1 Unit
Feature : Corrosionresistant, Compact design, Easy installation
Frequency : 50 Hz / 60 Hz
Purity Level : 90% and above (Ozone output)
Technology : Corona Discharge
Material : Stainless Steel 304/316
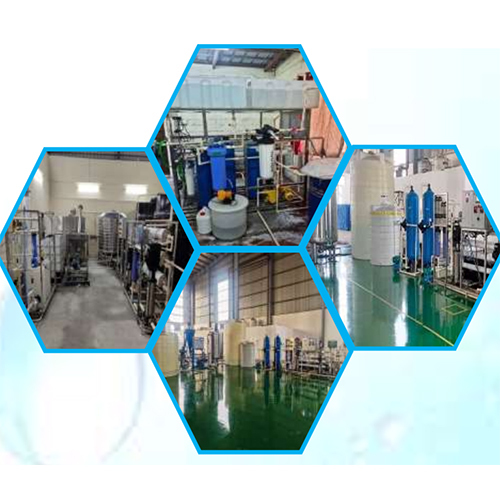
DEF-Urea-Adblue Plant
Minimum Order Quantity : 1 Unit
Feature : Corrosion resistant, low maintenance, PLC control
Frequency : 50/60 Hz
Purity Level : >32.5% Urea Solution
Technology : Reverse Osmosis, Ion Exchange, Mixing
Material : Stainless Steel 304/316

Developed and Managed by Infocom Network Private Limited.