Send Inquiry
Demineralization (DM) Plants
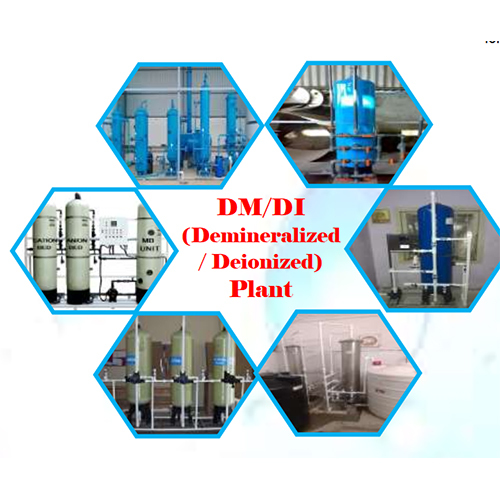

Demineralization (DM) Plants Specification
- Efficiency (%)
- 98-99%
- Pump Type
- Centrifugal / Dosing Pump
- Feature
- Corrosion Resistant, Fully/ Semi-Automatic, Easy Operation
- Noise Level
- Low (<60 dB)
- Recycle Rate
- Up to 95%
- Water Out Conductivity
- <0.5 S/cm
- Usage & Applications
- Industrial Boiler Feed, Laboratory, Process Water, Pharma, Electronics, Chemical Plants
- Flow Rate
- 500 LPH to 50000 LPH
- Frequency
- 50/60 Hz
- Power Consumption
- 2-10 kW depending on capacity
- Ph Level
- 6.5-7.5
- Technology
- Ion Exchange, Mixed Bed, Two Bed
- Automatic Grade
- Automatic / Semi-Automatic
- Volume
- Variable as per design (500 L to 50000 L)
- Material
- FRP, Stainless Steel, Mild Steel Rubber Lined
- Water Source
- Borewell, Municipal, Surface Water
- Purity Level
- 98-99%
- Drive Type
- Electric Motor
- Voltage
- 220-440 V
- Power Source
- Electric
- Product Type
- Demineralization / Deionization Plant
- Filter Type
- Multigrade/Pressure Sand/Carbon Filter
- Capacity
- 500 LPH to 50000 LPH
- Installation Type
- Containerized/ Skid Mounted/ Floor Mounted
- Resin Type
- Strong Acid Cation and Strong Base Anion Exchange Resin
- Design Temperature
- 5C to 45C
- Regeneration Chemical
- Acid and Alkali (HCl/NaOH)
- Total Dissolved Solids (TDS) removal efficiency
- 95-99%
- Inlet Hardness
- < 400 ppm as CaCO3
- Pre Filtration Requirement
- Yes (with sand/ carbon filter)
- Operating Pressure
- 2-4 kg/cm2
- Control Panel
- Microprocessor/PLC based (Optional)
- Outlet Silica Level
- <0.02 ppm
- Water in conductivity
- <800 S/cm
- Resin Life
- 2-4 years under standard conditions
Demineralization (DM) Plants Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 1 Unit Per Week
- Delivery Time
- 7 Days
About Demineralization (DM) Plants
Versatile Application & User Suitability
Demineralization (DM) Plants are recognized for their stellar use across various industries. Regularly used by manufacturers, exporters, and service providers, they are ideal for laboratory settings, pharmaceutical production, process water applications, chemical plants, and industrial boiler feed. Their robust construction offers suitability for floor, containerized, or skid-mounted installations, accommodating surfaces including FRP, stainless steel, and mild steel rubber-lined configurations. These systems are well-suited for both compact facilities and expansive industrial sites requiring dependable, high-purity water supply.
Prompt Delivery & Certified Quality
Expect competitive rates and reliable order completion with every Demineralization (DM) Plant purchase. Products are certified to stringent quality standards, ensuring consistent performance and safety. Sample units are available upon request, allowing for first-hand evaluation before a large order. From initial quotation to delivery, experience streamlined service, with options tailored to suit urgent project requirements. Our efficient order fulfillment and delivery times guarantee your operations continue seamlessly with minimal downtime.
FAQ's of Demineralization (DM) Plants:
Q: How does the demineralization process work in these DM Plants?
A: The DM Plants utilize strong acid cation and strong base anion exchange resins to remove minerals and dissolved solids from water. Water first passes through a pre-filtration system, then through the ion exchange resins, delivering water with ultra-low conductivity and high purity.Q: What are the primary usage areas for these DM Plants?
A: These DM Plants are used in diverse sectors such as industrial boiler feed water, laboratories, process water for manufacturing, pharmaceutical production, electronics, and chemical plants, ensuring purified water for sensitive and critical applications.Q: When should I consider regenerating the resins and how is it done?
A: Resin regeneration is typically required after a certain number of operating cycles, depending on water quality and usage. The process involves flushing the resins with acid (HCl) and alkali (NaOH) to restore their exchange capacity, which can usually be managed in-house or by a service provider.Q: What benefits do these DM Plants offer over other water treatment systems?
A: These DM Plants provide excellent removal of TDS and silica, consistent purity (98-99%), low operating costs, fast process cycles, flexible installation options, and can be customized for different flow rates and water sources, making them ideal for demanding applications.Q: Where can the DM Plants be installed and what surfaces are suitable?
A: The systems can be installed as containerized units, skid-mounted, or floor-mounted models, with a choice of corrosion-resistant materials. This makes them suitable for varied surfaces and facility layouts, from compact labs to large-scale industrial plants.
Price:
- 50
- 100
- 200
- 250
- 500
- 1000+

More Products in Water Solutions Category
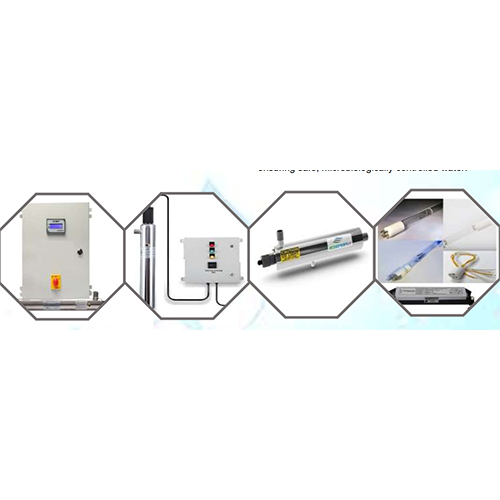
Ultraviolet (UV) Disinfection System
Minimum Order Quantity : 1 Unit
Technology : UVC Germicidal Irradiation
Product Type : Ultraviolet Disinfection System
Ph Level : Neutral (Does not alter pH)
Installation Type : Other , Floor/Wall Mounted
Power Consumption : 40500W (model dependent)
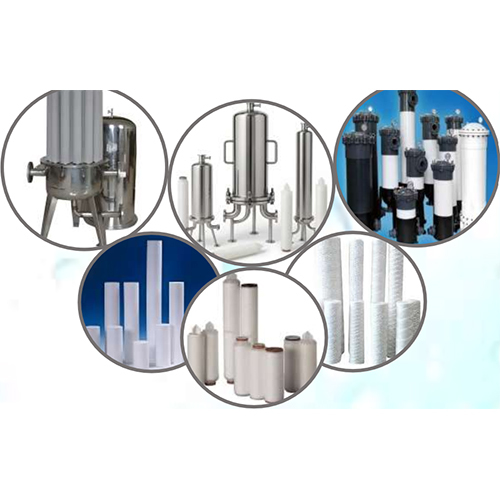
Micron Filtration Systems
Minimum Order Quantity : 1 Unit
Technology : Micron Filtration
Product Type : Micron Filtration System
Ph Level : Neutral output
Installation Type : Other , Vertical/Horizontal (Customizable)
Power Consumption : Low, depends on model
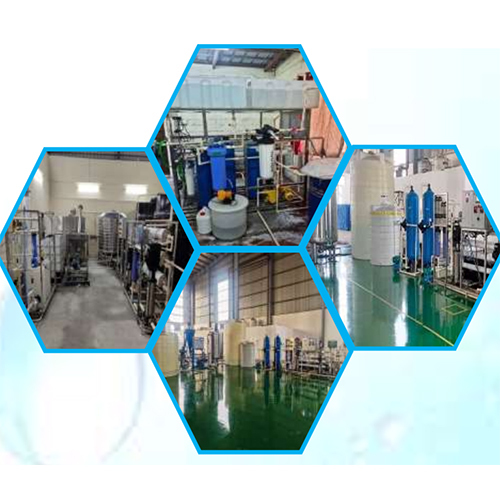
DEF-Urea-Adblue Plant
Minimum Order Quantity : 1 Unit
Technology : Reverse Osmosis, Ion Exchange, Mixing
Product Type : DEFUreaAdblue Plant
Ph Level : 710
Installation Type : Other , Skid Mounted/Fixed Installation
Power Consumption : 1035 kW (depending on capacity)
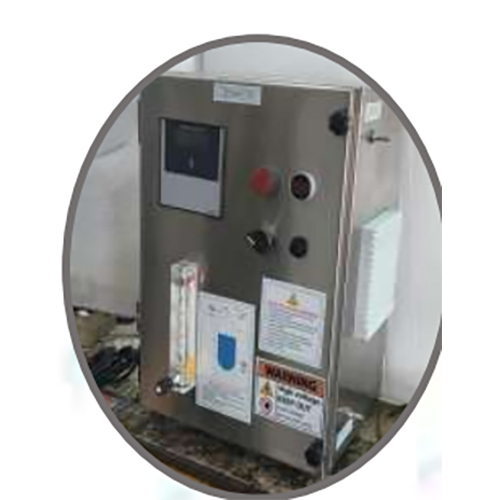
Ozone Generator
Minimum Order Quantity : 1 Unit
Technology : Corona Discharge
Product Type : Ozone Generator
Ph Level : N/A (Ozone generators affect water pH only temporarily)
Installation Type : Other , Floor Mounted / Wall Mounted
Power Consumption : 500 W to 5 kW (depends on model)

Developed and Managed by Infocom Network Private Limited.